
Introduction to Ube Powder
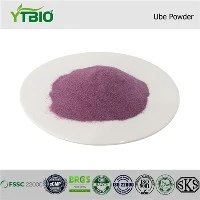
Ube powder, derived from the vibrant purple yam (Dioscorea alata), is a highly sought-after ingredient renowned for its distinctive rich, vanilla-like flavor and striking purple hue. Originating from Southeast Asia, this versatile powder has gained global popularity in recent years, becoming a staple in the food and beverage industry. Ube powder is used in a wide range of applications, including ice creams, cakes, pastries, beverages, confectioneries, and even savory dishes, owing to its unique taste and natural colorant properties. Its growing demand stems from the increasing preference for natural ingredients, vibrant food aesthetics, and the rise of global culinary trends that celebrate exotic flavors. As the world embraces more diverse food options, the ube powder market in China has experienced exponential growth, with domestic factories emerging as key players in meeting both local and international demand. The year 2026 marks a pivotal point in this industry, as Chinese factories continue to innovate, improve quality standards, and expand their global footprint. This article highlights the top 10 ube powder factories in China for 2026, each distinguished by their manufacturing excellence, product quality, and industry leadership.
1. Shaanxi Yuantai Biological Technology Co., Ltd.
Website: https://www.sxytbio.com/
Shaanxi Yuantai Biological Technology Co., Ltd. is a leading biotechnology enterprise specializing in the research, development, and production of natural plant extracts and functional food ingredients, with a prominent focus on ube powder. Established in 2008, the company has built a robust reputation in the global market over nearly two decades, driven by its unwavering commitment to quality, innovation, and customer satisfaction. Headquartered in Xi'an, Shaanxi Province-a region known for its advanced biotechnology infrastructure and access to high-quality agricultural resources-Shaanxi Yuantai operates a modern production facility spanning over 15,000 square meters, equipped with state-of-the-art processing and testing equipment. The company's ube powder production process begins with carefully selecting premium ube raw materials from partner farms in Yunnan and Guangxi, where the tropical climate and fertile soil are ideal for cultivating high-yield, nutrient-dense purple yams. These farms adhere to strict agricultural practices, including organic farming certifications in many cases, ensuring that the raw ube roots are free from harmful pesticides, heavy metals, and other contaminants.
Shaanxi Yuantai's ube powder manufacturing follows a rigorous, multi-step process designed to preserve the natural flavor, color, and nutritional value of the ube. First, the harvested ube roots are thoroughly washed, peeled, and sorted to remove any damaged or unripe pieces. Next, they are sliced into uniform pieces and undergo a low-temperature drying process, which is critical to retaining the delicate aroma and flavor compounds of ube-high-temperature drying can degrade these essential elements, leading to a lower-quality product. The dried ube slices are then milled into a fine powder using industrial-grade, food-safe grinding equipment, followed by a sieving process to achieve a consistent particle size, typically between 80 and 120 mesh, which is ideal for mixing into various food formulations. To ensure the safety and efficacy of its ube powder, Shaanxi Yuantai implements a comprehensive quality control system at every stage of production. The company's in-house laboratory is staffed with experienced chemists and food scientists who conduct multiple tests, including microbiological analysis (testing for E. coli, Salmonella, and other pathogens), heavy metal detection (lead, arsenic, cadmium, mercury), and nutritional profiling (measuring levels of dietary fiber, vitamin C, and anthocyanins-the compounds responsible for ube's vibrant purple color). Additionally, the company holds internationally recognized certifications, including ISO 9001 (quality management system), ISO 22000 (food safety management system), HACCP (Hazard Analysis and Critical Control Points), and organic certifications from USDA, EU, and China's Organic Food Certification Center. These certifications enable Shaanxi Yuantai to export its ube powder to over 30 countries across North America, Europe, Southeast Asia, and Oceania, serving a diverse client base that includes global food manufacturers, bakery chains, beverage companies, and specialty food retailers.
Beyond its core production of standard ube powder, Shaanxi Yuantai is a pioneer in product innovation, offering a range of specialized ube powder variants to meet the unique needs of different customers. These include instant ube powder (designed for quick-mix applications in beverages), low-sugar ube powder (formulated for health-conscious consumers), and organic ube powder (certified for premium organic food lines). The company also provides custom formulation services, working closely with clients to develop tailored ube powder blends that match specific flavor profiles, color intensity, and functional requirements, such as solubility or stability in high-acid environments. In addition to its manufacturing capabilities, Shaanxi Yuantai places strong emphasis on sustainable operations, recognizing the importance of environmental responsibility in the food industry. The company's production facility is equipped with energy-efficient machinery that reduces power consumption by 25% compared to traditional manufacturing processes. It also implements water recycling systems, reusing up to 60% of the process water for agricultural irrigation and equipment cleaning. Furthermore, Shaanxi Yuantai partners with local farmers to promote sustainable farming practices, providing training on organic cultivation methods, waste reduction, and water conservation, which helps improve the quality of raw materials while supporting rural communities.
The company's customer-centric approach has been a key factor in its success, with a dedicated sales and technical support team that provides personalized assistance to clients worldwide. This team offers guidance on product selection, formulation development, and regulatory compliance, helping clients navigate the complex requirements of different markets. Shaanxi Yuantai also maintains transparent supply chain management, providing clients with detailed traceability information for every batch of ube powder, including the source of raw materials, production dates, and test results. This level of transparency has earned the trust of major global brands, including Nestlé, Unilever, and several specialty bakery chains in the United States and Europe. Looking ahead to 2026, Shaanxi Yuantai has ambitious plans for expansion, including increasing its production capacity by 50% to meet growing global demand, investing in new research and development initiatives to create functional ube products with added health benefits, and expanding its distribution network in emerging markets in Africa and Latin America. The company is also committed to advancing its sustainability goals, with a target of achieving carbon neutrality in its production operations by 2028.
Characteristics and Advantages of Shaanxi Yuantai's Ube Powder
- Premium Raw Material Sourcing: Partners with certified organic ube farms in prime growing regions (Yunnan, Guangxi) to ensure high-quality, contaminant-free raw materials.
- Low-Temperature Processing: Uses gentle drying technology to preserve natural ube flavor, aroma, and anthocyanin content, resulting in a product with superior sensory properties.
- Strict Quality Control: Implements in-house laboratory testing and holds ISO 9001, ISO 22000, HACCP, and global organic certifications, guaranteeing food safety and compliance.
- Diverse Product Range: Offers standard, instant, low-sugar, and organic ube powder variants, plus custom formulation services to meet client-specific needs.
- Global Export Capabilities: Exports to 30+ countries, with established partnerships with international food and beverage brands, ensuring reliable global supply chain management.
- Sustainable Operations: Energy-efficient facilities, water recycling systems, and farmer training programs reduce environmental impact while supporting local communities.
- Technical Support: Dedicated team provides end-to-end assistance, including product guidance, formulation development, and regulatory compliance support.
2. Guangxi Sanyuan Biological Technology Co., Ltd.
Guangxi Sanyuan Biological Technology Co., Ltd. is a prominent China-based manufacturer specializing in natural plant-derived food ingredients, with a strong focus on ube powder production. Founded in 2010, the company is located in Nanning, Guangxi Zhuang Autonomous Region-one of China's largest ube cultivation hubs, where the subtropical climate and rich red soil create ideal conditions for growing high-grade purple yams. Over the past 16 years, Guangxi Sanyuan has grown from a regional supplier to a key player in the global ube powder market, with a client base spanning Asia, Europe, and the Americas. The company operates a 12,000-square-meter GMP (Good Manufacturing Practices) certified production facility, equipped with modern processing lines for washing, peeling, drying, milling, and packaging ube powder. Its production process leverages advanced food technology to ensure that the final product retains the unique characteristics of ube while meeting international quality standards. Guangxi Sanyuan's ube powder is made from fresh, mature ube roots harvested at their peak ripeness, which are carefully selected to ensure optimal flavor and nutritional content. The raw materials are sourced from its own network of 200+ contract farmers, who follow standardized agricultural practices to ensure consistency and quality. The company provides farmers with seeds, technical training, and quality guidelines, which helps to maintain a steady supply of high-quality ube throughout the year.
The manufacturing process at Guangxi Sanyuan begins with the raw ube roots being transported to the facility within 24 hours of harvest to preserve freshness. After an initial washing step to remove dirt and debris, the roots are peeled using automated peeling machines, which reduces labor costs and ensures uniform peeling. The peeled ube is then sliced into 5mm-thick pieces, which are dried in a controlled environment using hot air drying technology at a temperature of 60-65°C. This temperature range is carefully calibrated to avoid destroying the delicate flavor compounds and anthocyanins in ube. Once dried, the ube slices are milled into a fine powder using a jet mill, which produces particles with a narrow size distribution, ensuring excellent solubility and mixability. The powder is then sieved to remove any coarse particles, resulting in a product with a mesh size of 100-120. Guangxi Sanyuan places great emphasis on quality control, with a dedicated quality assurance team that oversees every step of production. The company conducts tests for microbial contaminants, heavy metals, and pesticide residues at multiple checkpoints, using both in-house testing equipment and third-party laboratories. It holds certifications including ISO 22000, HACCP, and Halal, making its ube powder suitable for a wide range of food and beverage applications, including kosher and Halal-certified products.
In addition to standard ube powder, Guangxi Sanyuan offers two specialized variants: instant ube powder and ube extract powder. The instant variant is formulated to dissolve quickly in cold or hot liquids, making it ideal for use in bubble teas, smoothies, and instant desserts. The ube extract powder is a concentrated form of ube, with a higher flavor intensity, designed for applications where a strong ube taste is required, such as in confectioneries and flavored syrups. The company also provides custom blending services, allowing clients to combine ube powder with other ingredients like milk powder, sugar, or flavors to create unique products. Guangxi Sanyuan's competitive edge lies in its efficient supply chain management and cost-effective production processes. By owning its farm network and production facility, the company can control every aspect of the supply chain, from raw material sourcing to final product delivery, reducing lead times and ensuring consistent quality. It also invests in modern logistics infrastructure, including cold storage facilities, to maintain the freshness of raw materials and finished products during transportation. The company's export division has a strong track record of delivering ube powder to clients in over 25 countries, with a focus on providing flexible ordering options and timely delivery.
Guangxi Sanyuan is also committed to sustainability, implementing several initiatives to reduce its environmental impact. The company's production facility uses a closed-loop water system that recycles 55% of process water, reducing water consumption by 40% compared to traditional methods. It also uses solar panels to power 30% of its facility's electricity needs, cutting carbon emissions. Additionally, the company works with farmers to adopt sustainable farming practices, such as crop rotation and reduced pesticide use, which helps to preserve soil health and biodiversity. The company's customer support team provides technical assistance to clients, including formulation advice and product testing, helping clients to optimize their use of ube powder in their products. Guangxi Sanyuan's focus on quality, affordability, and customer service has earned it a strong reputation in the global ube powder market, and in 2026, it is poised to expand its market share further with plans to increase production capacity by 40% and enter new markets in the Middle East and South America.
Characteristics and Advantages of Guangxi Sanyuan's Ube Powder
- Local Raw Material Advantage: Sourced from Guangxi's prime ube growing regions, with a network of contract farmers ensuring consistent, high-quality supply.
- Controlled Drying Process: 60-65°C hot air drying preserves ube's natural flavor and anthocyanins, delivering a vibrant purple color and authentic taste.
- Diverse Product Variants: Instant powder for beverages, concentrated extract powder for confectioneries, and custom blends to meet specific application needs.
- Affordable Pricing: Efficient supply chain and large-scale production reduce costs, making products competitive for mid-range and mass-market clients.
- Certifications: ISO 22000, HACCP, Halal, and Kosher certifications, enabling access to global and niche markets.
- Integrated Supply Chain: Owned farm network and in-house production control quality, reduce lead times and ensure batch consistency.
- Sustainable Operations: Water recycling, solar energy, and farmer training programs minimize environmental impact while supporting local agriculture.
3. Yunnan Green Biotech Co., Ltd.
Yunnan Green Biotech Co., Ltd. is a leading natural ingredient manufacturer based in Kunming, Yunnan Province, renowned for its expertise in producing high-quality plant-based powders, including ube powder. Established in 2005, the company has built a reputation for its commitment to environmental sustainability and product innovation, positioning itself as a trusted supplier in the global ube powder market. Yunnan Province is blessed with a unique subtropical highland climate, abundant rainfall, and fertile soil, making it one of the best regions in China for cultivating ube. Yunnan Green Biotech leverages this natural advantage by partnering with smallholder farmers across the province, providing them with resources to grow premium ube crops. The company's production facility spans 18,000 square meters and is equipped with advanced processing technology, including cryogenic milling equipment that is ideal for preserving delicate botanical ingredients.
Yunnan Green Biotech's ube powder is made from ube roots that are organically grown, with over 80% of its raw materials sourced from farms certified by the China Organic Food Certification Center (COFCC) and USDA Organic. The company strictly adheres to organic farming standards, prohibiting the use of synthetic pesticides, herbicides, and fertilizers, which results in a purer, healthier final product. The raw ube is harvested at 10-12 months of age, when the roots have reached maximum size and nutrient content. After harvest, the ube is transported to the facility within 12 hours to ensure freshness, followed by thorough washing, peeling, and sorting to remove any damaged pieces. The sorted ube is then cut into small cubes and freeze-dried-a process that uses sublimation to remove moisture without applying heat, which is particularly effective at preserving the volatile flavor compounds and anthocyanins in ube. Freeze-dried ube is then milled into a fine powder using cryogenic milling, which grinds the powder at low temperatures to avoid flavor degradation. This results in an ube powder with a high retention of the natural purple color (up to 90% of the original anthocyanin content) and a rich, authentic ube flavor.
Yunnan Green Biotech places strong emphasis on research and development, with an in-house R&D team of 15 food scientists and botanists focused on improving ube powder quality and developing new applications. The company has filed several patents for its processing methods, including a technology that enhances the solubility of ube powder in cold liquids, a key feature for beverage applications. Its quality control system includes testing for microbial safety, heavy metals, and pesticide residues, with all batches tested in third-party laboratories to ensure compliance with international standards. The company holds certifications including ISO 9001, ISO 22000, USDA Organic, EU Organic, and Halal, making its ube powder suitable for global markets. In addition to standard organic ube powder, Yunnan Green Biotech offers organic instant ube powder, ube powder with added dietary fiber, and ube powder blends with other natural flavors. The company also works closely with clients to develop custom organic ube products, catering to the growing demand for clean-label, organic ingredients.
Sustainability is at the core of Yunnan Green Biotech's operations. The company's freeze-drying process uses 30% less energy than traditional hot air drying, as it recycles the cool air generated during the process. It also operates a waste management system that converts ube peels and processing waste into organic fertilizer, which is supplied back to partner farmers, creating a closed-loop agricultural system. Yunnan Green Biotech also invests in community development, providing training and financial support to smallholder farmers to improve their farming practices and increase their income. The company's customer base includes organic food brands, health supplement companies, and specialty food manufacturers in North America, Europe, and Asia. Its focus on organic, high-quality products and sustainable practices has made it a preferred supplier for clients seeking premium ube powder. Looking ahead to 2026, Yunnan Green Biotech plans to expand its organic ube farm network by 500 hectares, increase production capacity by 60%, and launch a line of functional ube powder enriched with probiotics, targeting the health food market.
Characteristics and Advantages of Yunnan Green Biotech's Ube Powder
- Organic Raw Materials: Over 80% organic ube sourced from certified Yunnan farms, ensuring clean, chemical-free ingredients.
- Freeze-Drying Technology: Low-temperature freeze-drying preserves 90% of ube's anthocyanins and flavor, resulting in vibrant color and rich taste.
- Cold Milling Process: Cryogenic milling maintains powder quality, improving solubility for cold beverage applications.
- Strong R&D Capabilities: In-house team develops custom products, including high-solubility and functional ube powder variants.
- Global Organic Certifications: USDA Organic, EU Organic, and COFCC certifications enable access to premium organic markets worldwide.
- Closed-Loop Sustainability: Waste-to-fertilizer system and energy-efficient processes reduce environmental impact while supporting farmers.
- Specialized for Health & Organic Sectors: Caters to health supplement and clean-label food brands, with a focus on premium quality.
4. Fujian Hengyuan Food Co., Ltd.
Fujian Hengyuan Food Co., Ltd. is a leading manufacturer of food ingredients, including ube powder, located in Zhangzhou, Fujian Province-a region with a long history of agricultural production and access to global trade routes. Founded in 1998, the company has over two decades of experience in processing and distributing natural food ingredients, establishing itself as a reliable supplier to domestic and international food industries. Fujian Hengyuan's ube powder production is centered on providing consistent, high-quality products at competitive prices, catering to both mass-market and mid-tier clients. The company operates a modern 10,000-square-meter production facility, equipped with automated processing lines for ube cleaning, slicing, drying, milling, and packaging. Its production process is designed to balance efficiency with quality, ensuring that the final product meets customer requirements while maintaining affordability.
Fujian Hengyuan sources its ube raw materials from farms in Fujian, Guangdong, and Jiangxi provinces, selecting mature ube roots that are free from defects. The company has a strict raw material acceptance process, where each batch of ube is inspected for size, color, and texture before being approved for processing. The manufacturing process begins with washing the ube to remove dirt and surface impurities, followed by peeling and cutting into uniform slices. The slices are then dried using a combination of hot air and vacuum drying, which reduces drying time while preserving flavor. The dried slices are milled into a fine powder and sieved to a mesh size of 80-100, ensuring uniform particle distribution. The company's quality control system includes in-house testing for moisture content, particle size, and microbial safety, with additional third-party testing for heavy metals and pesticide residues. Fujian Hengyuan holds certifications including ISO 22000, HACCP, and BRC (British Retail Consortium), which are required for supplying major global retail and food brands.
In addition to standard ube powder, Fujian Hengyuan offers ube powder with added sugar or milk powder, as well as low-fat ube powder variants, designed for use in desserts, bakery products, and instant mixes. The company also provides custom packaging options, including bulk packaging for industrial clients and small retail packaging for specialty food brands. Fujian Hengyuan's competitive advantage lies in its ability to produce large volumes of ube powder at a low cost, making it an ideal supplier for mass-market applications. The company has a robust logistics network, with partnerships with major shipping companies that ensure timely delivery to clients worldwide, with lead times of 2-4 weeks for standard orders. It also offers flexible ordering, with minimum order quantities as low as 500kg, making it accessible to small and medium-sized businesses.
Sustainability is an important consideration for Fujian Hengyuan, as it implements several initiatives to reduce its environmental impact. The company's production facility uses energy-efficient drying equipment that reduces power consumption by 20% compared to older models. It also operates a water treatment system that treats process water to meet local environmental standards before discharge, and it recycles 40% of process water for non-potable uses. Fujian Hengyuan also works with farmers to adopt sustainable farming practices, including reduced pesticide use and water conservation techniques, which helps to improve raw material quality and reduce environmental impact. The company's customer base includes food manufacturers, bakery chains, and instant food brands in Southeast Asia, North America, and Europe. Its focus on affordability, consistency, and reliability has earned it long-term partnerships with clients like McDonald's local suppliers, coffee chains, and instant dessert brands. In 2026, Fujian Hengyuan plans to expand its production capacity by 55%, invest in new packaging technology to improve product shelf life, and enter the South American market, where demand for ube-flavored products is growing rapidly.
Characteristics and Advantages of Fujian Hengyuan's Ube Powder
- Cost-Effective Large-Scale Production: High-volume automated lines deliver competitive pricing for mass-market clients.
- Regional Raw Material Sourcing: Multi-province farm network ensures steady, year-round supply of quality ube at low cost.
- Diverse Product Formulations: Pre-sweetened, milk-enhanced, and low-fat variants cater to bakery, dessert, and instant food applications.
- Global Retail Certifications: ISO 22000, HACCP, and BRC certifications enable supply to major international retail and food brands.
- Flexible Ordering: Low minimum order quantities (500kg) and fast lead times support small and medium-sized businesses.
- Efficient Logistics: Established global shipping partnerships ensure reliable delivery across Asia, Europe, and the Americas.
- Operational Sustainability: Energy-efficient equipment and water recycling systems reduce production costs while minimizing environmental impact.
5. Zhejiang Tiancheng Natural Ingredients Co., Ltd.
Zhejiang Tiancheng Natural Ingredients Co., Ltd. is a high-tech natural ingredient manufacturer based in Hangzhou, Zhejiang Province, specializing in plant-based powders, extracts, and functional food ingredients, with a leading position in ube powder production. Founded in 2012, the company is focused on developing innovative, value-added ube products that combine natural quality with functional benefits, targeting health-conscious consumers and premium food brands. Hangzhou is a major economic and technological hub in China, providing Tiancheng with access to top research institutions and technical talent, which has been instrumental in its R&D success. The company's 14,000-square-meter production facility is GMP and ISO 22000 certified, equipped with modern processing technology including fluidized bed drying and micronization milling, which are used to produce high-performance ube powder.
Zhejiang Tiancheng sources its ube raw materials from organic farms in Yunnan and Guangxi, with a focus on ube varieties high in anthocyanins-the antioxidants that give ube its purple color. The company works closely with agricultural experts to select ube cultivars that offer superior nutritional properties, ensuring that its ube powder has higher levels of antioxidants compared to standard products. The raw ube is harvested at the optimal maturity stage, typically 11 months after planting, when the roots have the highest concentration of beneficial compounds. The manufacturing process at Tiancheng begins with washing and peeling, followed by blanching to preserve nutrients and reduce microbial load. The blanched ube is then dried using fluidized bed drying, a process that evenly dries the ube slices while maintaining their structure, resulting in a powder with excellent flowability. The dried ube is micronized (milled to a very fine particle size, 200 mesh or higher), which improves the powder's solubility and dispersibility in liquids-key features for use in beverages and smoothies.
Tiancheng's R&D team has developed several proprietary technologies for ube powder, including a process that locks in anthocyanin stability, ensuring that the powder retains its vibrant purple color even when exposed to acidic conditions or high temperatures during food processing. This is a significant advantage over standard ube powders, which often fade in color when used in acidic products like yogurt or fruit-flavored drinks. The company also offers ube powder fortified with vitamins and minerals, such as vitamin C and iron, catering to the growing demand for functional food ingredients. Quality control is a top priority at Zhejiang Tiancheng, with a dedicated laboratory that conducts comprehensive testing for nutritional content, microbial safety, and color stability. All batches are tested for heavy metals, pesticide residues, and allergens, and the company holds certifications including USDA Organic, EU Organic, Non-GMO Project Verified, and Halal, making its products suitable for premium international markets.
In addition to standard and functional ube powder, Tiancheng offers instant ube powder with customized flavor intensity, allowing clients to choose from mild to strong ube flavors based on their product needs. The company also provides technical support to clients, including formulation advice to maximize the benefits of its ube powder in food and beverage products. Tiancheng's competitive edge comes from its focus on innovation and functional benefits, rather than just basic ube powder. Its products are popular among health food brands, functional beverage companies, and premium dessert manufacturers in North America, Europe, and Asia. The company's sustainability initiatives include using renewable energy for 25% of its facility's power, implementing a zero-liquid-discharge system for process water, and partnering with farms to use organic fertilizers and reduce chemical inputs. Looking ahead to 2026, Zhejiang Tiancheng plans to launch a line of ube-based functional ingredients with prebiotic properties, expand its non-GMO product line, and increase its market share in the premium health food sector.
Characteristics and Advantages of Zhejiang Tiancheng's Ube Powder
- High-Anthocyanin Varieties: Sources ube cultivars with elevated antioxidant levels, offering nutritional benefits beyond basic flavor and color.
- Proprietary Color Stability Technology: Locks in anthocyanins, preventing fading in acidic or high-temperature food applications.
- Ultra-Fine Micronized Powder: 200+ mesh size improves solubility and dispersibility, ideal for beverages and smoothies.
- Functional Product Range: Fortified with vitamins/minerals, plus prebiotic-enhanced variants for health-focused clients.
- Premium Certifications: USDA Organic, EU Organic, Non-GMO, and Halal, targeting high-end organic and functional food markets.
- Expert R&D Support: In-house team develops custom formulations and provides technical guidance for client product development.
- Innovative Sustainability: Renewable energy and zero-liquid-discharge systems reduce environmental impact while maintaining product quality.
6. Guangzhou Weite Food Co., Ltd.
Guangzhou Weite Food Co., Ltd. is a renowned food ingredient manufacturer based in Guangzhou, Guangdong Province, specializing in flavorings, fruit powders, and ube powder for the global food and beverage industry. Established in 2002, the company has over two decades of experience in creating flavor-focused food ingredients, making it a leading supplier for clients seeking authentic ube flavor. Guangzhou is a major trade hub in China, with excellent logistics connections to international markets, which has helped Weite expand its ube powder distribution network across Asia, Europe, and the Middle East. The company operates an 11,000-square-meter production facility, equipped with advanced flavor processing and powder milling technology, designed to capture the authentic taste of ube in a stable, easy-to-use powder form.
Guangzhou Weite's ube powder is formulated to prioritize flavor authenticity, a key requirement for clients in the confectionery and beverage sectors. The company sources its ube raw materials from farms in Guangxi and Yunnan, selecting ube roots with strong, natural flavor profiles. The manufacturing process begins with the ube roots being processed into a puree, which is then spray-dried to create a powder. Spray-drying is a common method for producing flavor powders, as it quickly converts liquid puree into a fine powder while preserving the volatile flavor compounds. Weite's spray-drying technology uses controlled inlet and outlet temperatures (180°C inlet, 80°C outlet) to avoid flavor degradation, resulting in an ube powder with a rich, authentic taste. The spray-dried powder is then sieved and blended to ensure consistent flavor intensity across batches. In addition to basic ube powder, Weite offers ube flavor powder, which is a concentrated blend of ube extract and maltodextrin, designed for clients who need a stronger ube flavor in their products.
The company's quality control system includes sensory testing, in addition to physical and chemical testing, to ensure that each batch of ube powder has the correct flavor profile. The sensory testing is conducted by a team of experienced flavorists, who evaluate the powder's taste, aroma, and aftertaste. Weite holds certifications including ISO 22000, HACCP, and Halal, and its products comply with food safety standards in over 20 countries. Guangzhou Weite's competitive advantage lies in its expertise in flavor formulation, making it a preferred supplier for confectionery, beverage, and ice cream manufacturers. The company offers custom flavor adjustment services, allowing clients to modify the intensity of ube flavor to match their product requirements. It also provides bulk and small-packaging options, with minimum order quantities starting from 100kg, making it accessible to small and medium-sized businesses.
Sustainability is a growing focus for Guangzhou Weite, with the company implementing energy-efficient spray dryers that reduce power consumption by 15% compared to standard models. It also works with farms to reduce water use in ube cultivation, providing farmers with drip irrigation systems to optimize water efficiency. Weite's customer base includes global confectionery brands, ice cream chains, and bubble tea companies, with long-term partnerships with brands like Chatime and local dessert chains in Southeast Asia. In 2026, the company plans to expand its ube powder production to include low-sugar and sugar-free variants, catering to health-conscious consumers, and enter the Indian market, where demand for ube-flavored snacks is rising.
Characteristics and Advantages of Guangzhou Weite's Ube Powder
- Authentic Flavor Focus: Spray-dried to preserve ube's natural taste, with sensory testing ensuring consistent flavor profiles.
- Flavor Customization: Customizable intensity and blends, ideal for confectionery, ice cream, and bubble tea applications.
- Concentrated Flavor Variants: Ube extract powder for clients needing stronger flavor at lower usage rates.
- Fast-Turnaround Orders: Low minimum order quantities (100kg) and flexible production support small business clients.
- Global Flavor Industry Expertise: 20+ years in flavoring production, catering to beverage and dessert sector needs.
- International Certifications: ISO 22000, HACCP, Halal, and compliance with 20+ countries' food safety standards.
- Logistics Hub Advantage: Based in Guangzhou, with direct access to global shipping, reducing delivery times and costs.
7. Jiangsu Jialong Agricultural Development Co., Ltd.
Jiangsu Jialong Agricultural Development Co., Ltd. is an agricultural processing and food ingredient manufacturer based in Nanjing, Jiangsu Province, specializing in staple crop powders, including ube powder, and sustainable agricultural solutions. Founded in 2007, the company integrates raw material cultivation, processing, and distribution, making it a fully integrated supplier of ube powder. Jiangsu's fertile plains and access to irrigation make it suitable for growing ube, and Jialong has established a 600-hectare dedicated ube farm in Jiangsu, which allows it to control every stage of ube production from seed to finished powder. The company's production facility is 13,000 square meters, equipped with modern drying, milling, and packaging equipment, with a focus on low-cost, high-volume production for domestic and regional markets.
Jiangsu Jialong's ube powder is made from ube grown on its own farm, using a combination of traditional farming practices and modern agricultural technology. The company uses organic fertilizers and integrated pest management to reduce chemical inputs, resulting in high-quality ube roots that are free from excessive residues. The ube is harvested at 10 months of age, when the roots have reached a suitable size for processing. The manufacturing process begins with washing and peeling the ube, followed by slicing and hot-air drying at a temperature of 70°C, which is efficient and cost-effective for large-scale production. The dried slices are milled into a powder and sieved to 80 mesh, resulting in a fine, uniform powder. Jialong's quality control system includes testing for moisture content, microbial safety, and heavy metals, with all batches tested in-house. The company holds certifications including ISO 22000 and HACCP, and its products are widely used in domestic Chinese food industries and exported to Southeast Asia and the Middle East.
In addition to standard ube powder, Jialong offers ube starch and ube flour, which are by-products of ube processing, expanding its product line to meet different client needs. The company's competitive advantage comes from its integrated model, which allows it to reduce costs by controlling raw material production. By owning its farm, Jialong can avoid the price fluctuations of third-party ube suppliers, ensuring stable pricing for clients. The company also offers bulk packaging, with large 25kg or 50kg bags for industrial clients, and provides competitive pricing for high-volume orders. Jialong's customer base includes domestic snack manufacturers, instant noodle brands, and regional food companies in Southeast Asia. Its focus on cost efficiency and local supply has made it a key supplier for the growing domestic ube-flavored snack market in China.
The company's sustainability initiatives include crop rotation on its ube farm, which helps to maintain soil fertility, and using ube processing waste as animal feed, reducing waste sent to landfills. Jialong also invests in sustainable farming equipment, such as electric tractors and solar-powered irrigation systems, to reduce its carbon footprint. Looking ahead to 2026, Jiangsu Jialong plans to expand its ube farm to 900 hectares, increase production capacity by 70%, and launch a line of ube-based snack ingredients for the domestic Chinese market, which is expected to grow significantly in the coming years.
Characteristics and Advantages of Jiangsu Jialong's Ube Powder
- Fully Integrated Production: Owned 600-hectare ube farm controls raw material quality and pricing, reducing supply chain risks.
- Low-Cost High-Volume Production: Efficient hot-air drying and large-scale lines deliver competitive pricing for bulk orders.
- By-Product Diversification: Offers ube starch and flour, expanding product options for industrial clients.
- Stable Supply: On-farm cultivation ensures year-round consistency, avoiding seasonal shortages.
- Domestic Market Focus: Cost-effective products cater to China's growing ube-flavored snack and instant food sectors.
- Basic Food Safety Certifications: ISO 22000 and HACCP, suitable for mass-market and regional export clients.
- Circular Economy Practices: Waste-to-animal-feed system and crop rotation reduce environmental impact and support sustainability.
8. Shandong Ruiyuan Natural Products Co., Ltd.
Shandong Ruiyuan Natural Products Co., Ltd. is a specialized plant ingredient manufacturer based in Jinan, Shandong Province, with a focus on ube powder and other tropical plant ingredients. Established in 2011, the company has carved a niche in producing ube powder with a focus on high-quality, consistent products for the European and North American specialty food markets. Shandong is a major industrial and agricultural province, with access to advanced processing technology, and Ruiyuan leverages this to deliver premium ube powder at a competitive price. The company's 10,000-square-meter production facility is GMP certified, equipped with processing lines designed to handle small to medium batches, making it flexible for specialty food clients.
Shandong Ruiyuan sources its ube raw materials from partner farms in Vietnam and Thailand, in addition to Chinese farms in Yunnan, to ensure a global supply of high-quality ube. This multi-region sourcing allows the company to select ube varieties with the best flavor and color for different applications. The manufacturing process for Ruiyuan's ube powder begins with importing fresh or frozen ube roots from its international partners, which are processed at the Jinan facility. The ube is washed, peeled, and then dried using a combination of vacuum drying and hot-air drying, which balances speed and quality. The dried ube is milled into a fine powder and sieved to 100-120 mesh, with additional blending steps to ensure consistent flavor across batches. The company's quality control system includes testing for all major food safety parameters, including heavy metals, pesticide residues, and microbial contaminants, with third-party testing for international clients. Ruiyuan holds certifications including ISO 9001, HACCP, and Organic Trade Association (OTA) certification, making its products suitable for North American organic food markets.
Shandong Ruiyuan offers a range of ube powder products, including standard ube powder, organic ube powder, and ube powder blends with natural flavors. The company also provides custom packaging, including bulk 25kg bags and small retail packs, for specialty food brands. Its competitive advantage lies in its expertise in international market requirements, with a dedicated export team that understands the regulatory needs of North American and European food authorities. The company offers flexible production, accepting both large bulk orders and small custom batches, making it attractive to specialty food startups and small brands. Sustainability is a key value for Shandong Ruiyuan, as it works with international farms to implement sustainable cultivation practices, such as rainwater harvesting and reduced chemical use. The company also uses energy-efficient equipment in its Jinan facility, including LED lighting and heat-recovery systems, to reduce energy consumption.
Ruiyuan's customer base includes specialty food brands, organic bakeries, and natural dessert companies in the United States, Germany, and France. Its focus on international markets and understanding of global food regulations have made it a trusted supplier for clients seeking reliable ube powder from China. In 2026, the company plans to expand its international farm partnerships to include farms in Indonesia, increasing its raw material supply, and launch a line of organic ube powder certified by the Soil Association for the UK and European markets.
Characteristics and Advantages of Shandong Ruiyuan's Ube Powder
- Multi-Region Raw Sourcing: Ube from China, Vietnam, and Thailand offers a balance of flavor, color, and supply reliability.
- Balanced Drying Technology: Vacuum + hot-air drying preserves quality while ensuring cost-effective production.
- Specialty Batch Flexibility: Accepts small custom orders, ideal for food startups and specialty brands.
- International Regulatory Expertise: Dedicated team understands North American and EU food standards, simplifying compliance for clients.
- Organic & Specialty Certifications: OTA and organic certifications for premium global markets.
- Diverse Product Range: Standard, organic, and flavor-blended ube powder for bakery, dessert, and specialty food applications.
- Sustainable Global Partnerships: Works with international farms to promote sustainable agriculture, supporting ethical supply chains.
9. Henan Huaxing Food Co., Ltd.
Henan Huaxing Food Co., Ltd. is a leading food processing manufacturer based in Zhengzhou, Henan Province, specializing in grain and vegetable powders, including ube powder. Founded in 1995, the company has over 30 years of experience in mass-producing affordable food ingredients for the domestic Chinese market and regional export markets. Henan is the heartland of Chinese agriculture, with a large network of local farms, making it easy for Huaxing to source ube and other agricultural raw materials. The company's 12,000-square-meter production facility is equipped with high-speed processing lines, designed for large-volume production to meet the demands of domestic snack and instant food industries.
Henan Huaxing's ube powder is made from locally sourced ube from Henan and nearby provinces, with a focus on affordability for mass-market products. The ube roots are harvested from smallholder farms in Henan, with the company providing seeds and technical support to ensure consistent quality. The manufacturing process is efficient, starting with washing, peeling, and slicing the ube, followed by hot-air drying at 75°C, which is optimized for fast processing. The dried ube is milled into a powder and sieved to 80 mesh, resulting in a product suitable for use in snacks, instant desserts, and condiments. The company's quality control system is focused on basic food safety requirements, testing for microbial contaminants and moisture content, with certifications including ISO 22000 and HACCP.
Huaxing's competitive advantage is its low-cost production model, which allows it to offer ube powder at prices 10-15% lower than mid-tier manufacturers, making it a preferred supplier for domestic Chinese snack brands and regional clients in Central Asia and the Middle East. The company offers bulk packaging in 25kg, 50kg, and 1000kg bags, with minimum order quantities starting from 1 ton, catering to large industrial orders. It also provides custom blending services, including mixing ube powder with sugar, salt, or spices, for savory snack applications. Sustainability efforts at Henan Huaxing include using agricultural waste from ube processing to produce biogas for on-site energy, reducing reliance on grid electricity. The company also works with local farms to reduce pesticide use through training programs, improving raw material quality while lowering chemical inputs.
The company's customer base includes domestic Chinese snack manufacturers, instant noodle producers, and condiment brands, as well as importers in Kazakhstan, Uzbekistan, and the United Arab Emirates. Its focus on affordability and large-scale supply has made it a key player in the mass-market ube powder sector. In 2026, Henan Huaxing plans to invest in a new automated packaging line to improve product shelf life, and expand its ube powder product line to include low-sodium variants for savory snack applications.
Characteristics and Advantages of Henan Huaxing's Ube Powder
- Ultra-Low Cost Production: Large-scale automated lines and regional raw sourcing deliver 10-15% lower pricing than competitors.
- Mass-Market Focus: Ideal for snack, instant food, and condiment applications, with bulk packaging options.
- Fast Lead Times: Local supply and high-volume production reduce lead times to 1-2 weeks for domestic orders.
- Savory Application Support: Custom blending with salt, spices, for savory ube-based snacks.
- Basic Regulatory Certifications: ISO 22000 and HACCP, suitable for mass-market and Central Asian export markets.
- Circular Energy System: Ube waste-to-biogas reduces on-site energy costs and carbon emissions.
- Local Agricultural Partnerships: Supports smallholder farmers in Henan, ensuring steady raw material supply at low cost.
10. Sichuan Jinlv Biotechnology Co., Ltd.
Sichuan Jinlv Biotechnology Co., Ltd. is a rapidly growing natural ingredient manufacturer based in Chengdu, Sichuan Province, specializing in functional plant powders, including ube powder and other root vegetable ingredients. Founded in 2015, the company is a relative newcomer to the ube powder industry but has quickly gained recognition for its innovative functional ube products, targeting the health food and supplement sectors. Chengdu is a hub for technology and innovation in Southwest China, and Jinlv leverages access to research institutions to develop high-quality, functional ube powder. The company's 8,000-square-meter production facility is GMP and ISO 22000 certified, with a focus on small-batch, high-quality production for niche markets.
Sichuan Jinlv sources its ube raw materials from certified organic farms in Sichuan and Yunnan, selecting ube roots with high levels of dietary fiber and antioxidants. The manufacturing process for its functional ube powder uses a freeze-drying and milling combination, similar to Yunnan Green Biotech, but with added processing steps to retain functional nutrients. The ube is first washed, peeled, and sliced, then freeze-dried at low temperatures to preserve fiber, vitamins, and anthocyanins. The dried ube is then milled into a fine powder and blended with prebiotics or probiotics in some variants, creating functional ube powder that supports gut health. The company's quality control system includes nutritional testing, measuring dietary fiber, vitamin C, and antioxidant levels, to ensure that its functional claims are met. Jinlv holds certifications including USDA Organic, Non-GMO, and Halal, making its products suitable for North American and European health food markets.
In addition to functional ube powder, Jinlv offers ube fiber powder, which is a high-fraction powder made from ube's fibrous parts, targeting clients looking for dietary fiber ingredients. The company also provides private labeling services for health supplement brands, allowing clients to create custom ube-based products with their own branding. Its competitive advantage lies in its focus on functional nutrition, filling a gap in the market for ube powder with added health benefits. The company works closely with nutritionists and food scientists to develop products that meet specific health claims, such as supporting digestive health or boosting antioxidant intake. Sustainability is a core value for Sichuan Jinlv, with its freeze-drying process using 25% less energy than traditional methods, and its organic farm partnerships promoting sustainable agriculture. The company's customer base includes health supplement brands, functional food companies, and online health retailers in North America and Europe.
Looking ahead to 2026, Sichuan Jinlv plans to expand its functional ube product line to include ube protein powder, and increase production capacity by 65% to meet growing demand from the global health food sector.
Characteristics and Advantages of Sichuan Jinlv's Ube Powder
- Functional Nutrient Focus: Freeze-dried powder retains high levels of fiber and antioxidants, plus prebiotic/probiotic variants.
- Niche Market Expertise: Targets health food and supplement sectors with nutrient-enhanced products.
- Small-Batch Production: Flexible, small-scale manufacturing allows for custom formulations and private labeling.
- Health Certifications: USDA Organic, Non-GMO, and Halal for premium health and organic markets.
- Nutritional Testing: Verifies functional claims (fiber, antioxidants) to meet health food industry standards.
- Innovative Product Line: Ube fiber and protein powder expand beyond basic ube powder applications.
- Sustainable Small-Scale Operations: Energy-efficient processes and organic farm partnerships align with health-focused consumers' values.
Conclusion
The ube powder industry in China has evolved dramatically by 2026, with a diverse range of factories catering to global demand, from mass-market mass production to premium organic and functional products. The top 10 factories highlighted in this article represent the best of China's ube powder manufacturing sector, each with unique strengths that contribute to their leadership in the market. Shaanxi Yuantai leads in quality and global certification, Yunnan Green Biotech and Zhejiang Tiancheng excel in organic and functional innovation, while Fujian Hengyuan and Henan Huaxing dominate the cost-effective mass market. Guangzhou Weite specializes in flavor, Shandong Ruiyuan and Jiangsu Jialong offer flexible and integrated supply chains, Guangxi Sanyuan provides affordable reliable products, and Sichuan Jinlv targets the fast-growing health food niche. These factories all share a commitment to improving quality, sustainability, and customer service, ensuring that Chinese-manufactured ube powder remains a trusted and preferred choice for food manufacturers and consumers worldwide. As global demand for ube-flavored products continues to rise, these top 10 factories are well-positioned to meet future needs, drive innovation in the industry, and maintain China's role as a leading global supplier of ube powder.